A rising-stem gate valve for isolation, with ANSI 150# flange ends, 2″–6″ (DN50–DN150), in Cast iron ASTM A126 B. Rated 150#, built to ASME B16.10 and tested to API 598. Graphite packed — isolation duty only, never throttling.
Tell us the size, the fluid, pressure and temperature — quotes within 2 working hours.
| Ends | ANSI 150# flange |
|---|---|
| Size | 2″–6″ (DN50–DN150) |
| Body | Cast iron ASTM A126 B |
| Pressure | 150# |
| Max temperature | not stated |
| Design | ASME B16.10 |
| Inspection | API 598 |
| Stem | Rising stem, handwheel, multi-turn |
| Packing | Graphite |
Isolation duty, ANSI 150# flange ends, built to ASME B16.10.
A rising-stem gate valve in 2″–6″ (DN50–DN150), body in Cast iron ASTM A126 B, rated 150#, inspected and tested to API 598. Fully open, the gate lifts clear of the bore and the valve presents almost no restriction and almost no pressure drop. That is what a gate valve is for.
The cheapest body in the range, and the only one that publishes no working temperature at all.
Held part-open, flow across the partly-raised gate vibrates it and erodes both gate and seat — permanently. Use a globe valve to regulate flow.
Metal-to-metal seating and a graphite-packed stem, rather than a PTFE seat. That is why gate valves take steam and hot oil where a ball valve stops at 150 °C.
As published. We print the catalogue figure rather than inferring one from a sibling variant.
The stem travels up out of the bonnet as the valve opens, so it needs more headroom open than closed. Handwheel operated — not a quarter turn.
The one standard common to every variant in this range, which is what makes their test pressures directly comparable.
The end type is the first decision and cannot be changed later. Check it against the pipework, not the pressure rating — all ten variants compared.
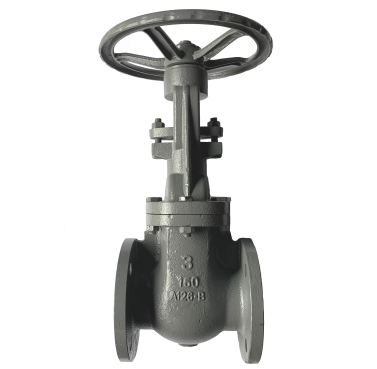
All photographs of the stocked item, not renders.
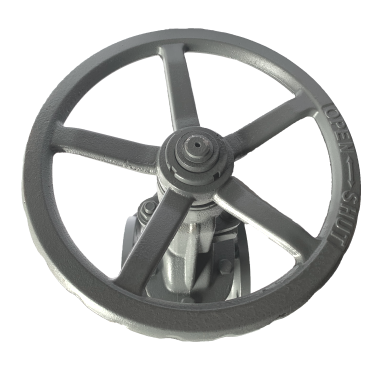
A rising-stem gate valve with the handwheel fitted. The stem you see above the bonnet is what travels as the valve opens — allow for it when you check headroom.
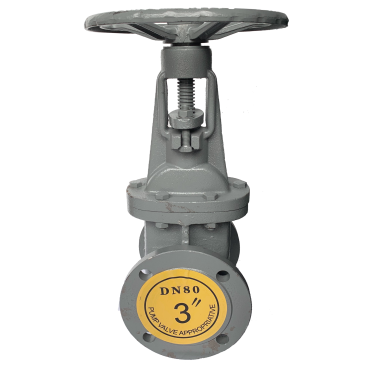
The end connection is the first thing to check against your pipework, and the one thing that cannot be changed after ordering.
Where the graphite packing sits. A small re-tighten of the gland after the first heat cycle is normal, not a fault.
Everything that goes on a purchase order.
| Item | Detail |
|---|---|
| Size range | 2″ to 6″ (DN50 to DN150) |
| End type | ANSI 150# flange — to ASME B16.1 |
| Body material | Cast iron ASTM A126 B |
| Working pressure | 150# |
| Maximum working temperature | ≤ 205 °C |
| Design and manufacture | ASME B16.10 |
| Inspection and test | API 598 |
| Shell or body test | 2.06 MPa |
| Seal test | 1.57 MPa |
| Gas tightness test | 0.6 MPa |
| Stem | Rising stem, handwheel operated, multi-turn |
| Packing | Graphite |
| Duty | Isolation only — never for throttling. For throttling use globe valves |
| Stock | Singapore & Malaysia warehouses — out within 24 hours |
Millimetres. Face-to-face L is the gap the valve needs in the run; on a rising-stem gate valve you also need headroom above it, because the stem travels up as it opens.
| Size | Part no | Bore d | Face-to-face L | O | Handwheel W | R | Bolts n-z | Flange thk t | RF height f | Weight (kg) |
|---|---|---|---|---|---|---|---|---|---|---|
| 2″ | VL-CI-GA-F-150-32 | 50 | 178 | 152 | 120 | 92.1 | 4-Ø19 | 15.5 | 2 | 14.80 |
| 2 1/2″ | VL-CI-GA-F-150-40 | 65 | 190 | 178 | 139 | 104.8 | 4-Ø19 | 16.6 | 2 | 20.10 |
| 3″ | VL-CI-GA-F-150-48 | 80 | 204 | 190 | 150 | 127 | 4-Ø19 | 18 | 2 | 34.00 |
| 4″ | VL-CI-GA-F-150-64 | 100 | 229 | 227 | 190 | 157.2 | 8-Ø19 | 22.5 | 2 | 39.00 |
| 5″ | VL-CI-GA-F-150-80 | 125 | 254 | 254 | 216 | – | 8-Ø22 | 23.9 | 2 | 50.30 |
| 6″ | VL-CI-GA-F-150-96 | 150 | 270 | 279 | 241.5 | – | 8-Ø22 | 25.4 | 2 | 61.15 |
This is a rising stem: the stem travels up out of the bonnet as the valve opens, so the space it needs open is greater than its closed height. Check the clearance before fitting it under a platform or in a duct.
Measure the gap in the run against it. On a replacement, measure the valve coming out rather than trusting a drawing — and remember a globe valve of the same size is longer.
Where a letter is ambiguous or mislabelled in the catalogue we say so rather than guess at what was meant.
A valve must not hang on the pipework, and must never be used to pull a misaligned joint together.
ANSI 150# flange — the end type is the first decision and cannot be changed after ordering.
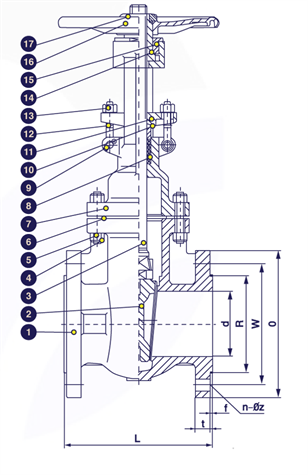
Seventeen callouts, and seventeen items in the parts list below — they correspond one to one. The dimension letters are the ones used in the size table: d bore, L face-to-face, O flange OD, W handwheel, R bolt circle, t flange thickness, f raised face and n–Øz the bolt pattern.
The callout numbers are the item numbers in the parts list below, and the dimension letters are the column headings in the size table above. Nothing on the drawing is named only there.
You can see it sitting clear of the bore when open. That is the gate valve advantage — almost no restriction — and the reason it must never be held part-open, because flow across a partly-raised wedge erodes both faces.
It is a catalogue section, not a manufacturing drawing: it carries no tolerances and no material callouts. Order spares by item number against the parts list.
The manufacturer’s item numbers, so a spares order matches the parts list.
| No | Part name | Material |
|---|---|---|
| 1 | Body | A126 B Cast Iron |
| 2 | Wedge | A126 B Cast Iron |
| 3 | Stem | A276 SS304 |
| 4 | Bolts | A29 1035 |
| 5 | Nuts | A29 1025 |
| 6 | Gasket | SS304 + Graphite |
| 7 | Bonnet | A126 B Cast Iron |
| 8 | Packing | Flexible Graphite |
| 9 | Pin | A29 1045 |
| 10 | Packing Gland | A276 SS304 |
| 11 | Gland Flange | A126 B Cast Iron |
| 12 | Eye Bolts | A29 1035 |
| 13 | Nuts | A29 1025 |
| 14 | Stem Nut | A276 SUS410 |
| 15 | Cover | A29 1025 |
| 16 | Handwheel | A47 32510 Malleable Iron |
| 17 | Nut | A29 1025 |
They match the callouts on the sectional drawing, so a spares order matches the section rather than a description.
Everything else is a casting or a fastener. On an isolation valve those two surfaces take the duty every time it is closed.
It is also the part that beds in. A small re-tighten of the gland after the first heat cycle is normal.
A bent or scored stem is the usual reason a gate valve will not seat, and it is the part that moves furthest every cycle.
If you need to know what touches your fluid, the whole list is above — we have not summarised it.
Factory proof tests. Not working pressures — the shell test proves the body, the seal test proves the gate against its seat. Do not design to them.
| Item | Value |
|---|---|
| Normal Pressure | 150# |
| Hydraulic Body Test | 2.06 MPa |
| Seal Test | 1.57 MPa |
| Hermetical Seal Test | 0.6 MPa |
The shell test proves the body and the seal test proves the gate against its seat. They are proof tests well above the working rating, and the valve is not intended to operate there.
That is the number to design to, at not stated.
Every variant in this range is inspected and tested to it, so the figures on the other nine pages can be read against these directly.
It is being run part-open. Throttling on the gate face erodes gate and seat permanently, and a wrecked seat will not shut off when you need it.
EN 10204 3.1 is available on request and the castings carry heat numbers — ask with the order, not after the goods arrive.
End type first, then the standard, then the material.
All ten side by side: the comparison table.
Isolation — fully open or fully shut. A rising-stem gate valve with ANSI 150# flange ends in 2″–6″ (DN50–DN150), body in Cast iron ASTM A126 B, rated 150#, built to ASME B16.10 and tested to API 598. Fully open it presents almost no restriction and almost no pressure drop.
No. Held part-open, flow across the partly-raised gate vibrates it and erodes both gate and seat — and the damage is permanent. A wrecked seat cannot be relied on to shut off. Use a globe valve to regulate flow.
Rated ≤ 205 °C, as printed in the manufacturer’s catalogue. The packing is graphite and the seating is metal to metal, which is what allows the heat — a PTFE-seated ball valve stops at 150 °C.
2″–6″ (DN50–DN150). Part numbers, the bill of materials and the test pressures are all on this page, as printed in the catalogue.
More than its closed height. This is a rising stem: the stem travels up out of the bonnet as the valve opens. Check the clearance before fitting it under a platform or in a duct.
We hold it in our Singapore and Malaysia warehouses, out of the warehouse within 24 hours of PO. Quotes within 2 working hours.
A gate valve isolates: fully open or fully shut. A globe valve throttles — it is built to run part-open, which a gate valve is destroyed by. If the valve will ever be adjusted, it must be a globe valve. Note the globe is also longer face-to-face, so the two are not interchangeable in the run.
Designed and manufactured to ASME B16.10, and inspected and tested to API 598. API 598 is the common thread across all ten variants, which is what makes their test pressures directly comparable.
It is handwheel operated and multi-turn, not quarter turn. Operating torque, the number of turns and any ISO 5211 pad are not published for this range — settle the actuation arrangement with us rather than assuming a top plate.
No Cv, no operating torque or turn count, no ISO 5211 pad, and no fire-safe certificate. EN 10204 3.1 certificates are available on request and the castings carry heat numbers. Anything the catalogue does not state we get from the factory rather than infer from a sibling variant.
Related: all gate valves · globe valves · ball valves · all low pressure valves
Baca halaman ini dalam Bahasa Indonesia